Bakery Pack Weight Control
Bakery Pack Weight Control is the production practice of measuring and managing the food quantity in finished packages against the declared net quantity and the bakery’s operating targets.
In Short
- Bakery Pack Weight Control is the production practice of measuring and managing the food quantity in finished packages against the declared net quantity and the…
- For FDA-regulated packaged foods, 21 CFR 101.7(a) requires a net quantity declaration on the principal display panel.
- The basic calculation is net weight = gross weight − tare weight.
It connects reliable weighing, representative packaging tare, sampling, process adjustment, and product disposition. The central question is not simply whether a scale displays the right number, but what that number represents and which packages the evidence supports.
1. Define the package and the control question
Bakery Pack Weight Control is the production practice of measuring and managing the food quantity in finished packages against the declared net quantity and the bakery’s operating targets. It connects reliable weighing, representative packaging tare, sampling, process adjustment, and product disposition. The central question is not simply whether a scale displays the right number, but what that number represents and which packages the evidence supports.
This guide concerns US packaged bakery foods, principally products controlled by net weight. It is distinct from bakery recipe control: correctly weighing flour into a mixer does not establish the net contents of a cooled, sliced, wrapped loaf. Ingredient accuracy, baking losses, portioning, and finished-package quantity are connected but separate control questions.
| Term | Meaning in production control | Important distinction |
|---|---|---|
| Declared or nominal net quantity | The food quantity stated on the package | Not the machine setpoint |
| Site target | The operating quantity selected for a defined process stage | Not a legal tolerance |
| Gross weight | Food plus the packaging being weighed | Not food weight alone |
| Tare weight | Packaging and other excluded material deducted from gross | Must represent the weighed configuration |
| Net weight | Gross weight minus tare weight | Meaning depends on measurement quality and timing |
| Production sample | Packages selected to understand current production | Not automatically a legal inspection sample |
Define the saleable unit before choosing targets. A bag of rolls, a loaf with a closure, a cake on a board, and a carton containing individually wrapped pastries have different packaging boundaries. Record which components are food, which are tare, and whether the measurement concerns an inner pack or the complete retail unit. Weight alone also does not establish a declared piece count.
Operational methods, diagrams, decision tables, and checklists below are suggested production practices unless explicitly identified as law or Handbook guidance. Assign responsibility for measurement, adjustment, holding stock, and release review. A line rejection is an equipment action under configured settings; deciding what happens to that product is a separate responsibility.
2. Separate FDA law from NIST inspection procedures
For FDA-regulated packaged foods, 21 CFR 101.7(a) requires a net quantity declaration on the principal display panel. It generally specifies weight for solid, semisolid, or viscous foods, subject to the exceptions stated in that provision. Paragraph (g) requires the declaration to reveal the food quantity exclusive of wrappers and other material packed with it. These are legal provisions, not optional production recommendations.
Paragraph (q) requires an accurate statement of contents. It recognizes reasonable variations caused by moisture loss or gain during good distribution practice or unavoidable deviations in good manufacturing practice, while stating that variations must not be unreasonably large. That wording is not permission to choose an arbitrary shortage allowance, nor does it make an internal target the legal declaration.
NIST Handbook 133, Checking the Net Contents of Packaged Goods, is a technical procedural guide for compliance testing. It is recommended for state adoption; its applicable adoption and use depend on the regulator and jurisdiction. Publication by NIST does not itself create a single nationwide bakery inspection law. Establish the responsible authority, applicable requirements, and inspection procedure for the product and location.
Handbook 133 distinguishes an average requirement from an individual-package requirement. Its Maximum Allowable Variation, or MAV, concerns an individual deficiency beyond which the error is considered unreasonable; the applicable sampling plan also matters. A sample average above the declaration therefore does not establish that the whole lot passes. Conversely, a reading below the declaration is not automatically an MAV violation.
3. Make gross, net, and tare measurements defensible
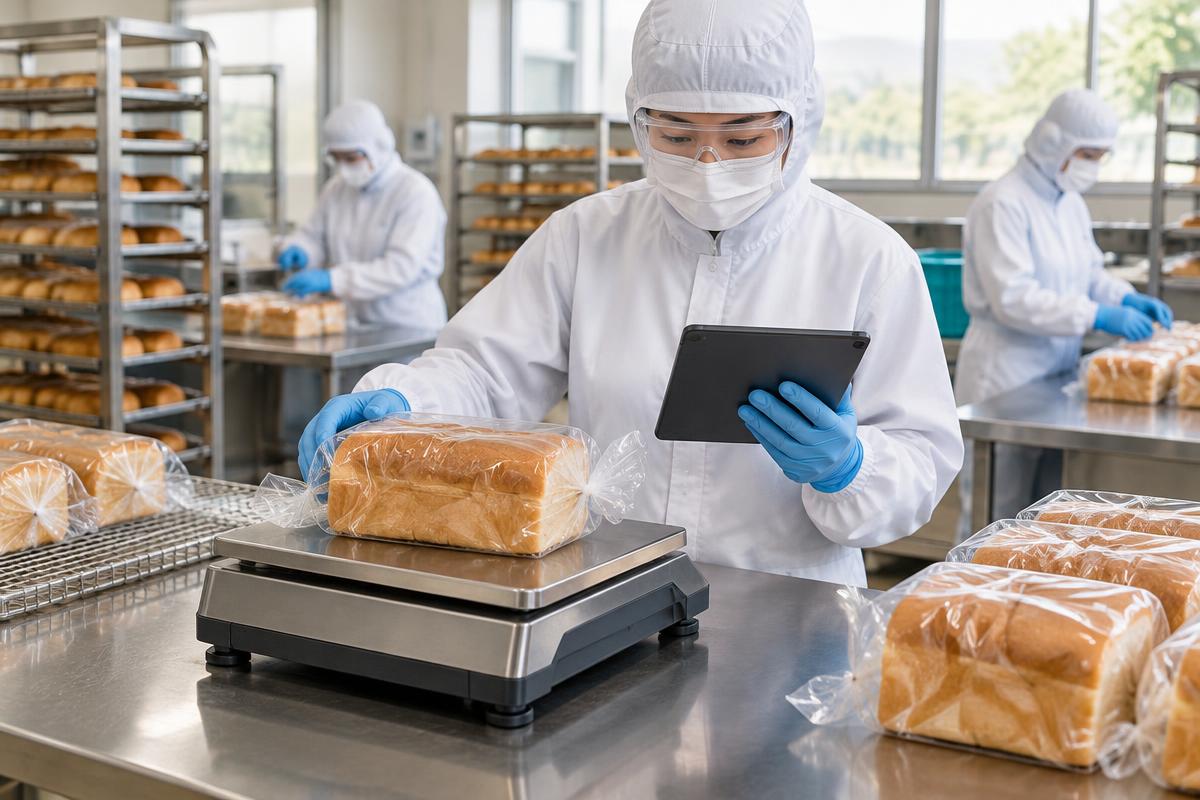
The basic calculation is net weight = gross weight − tare weight. In a fictional production measurement, a wrapped loaf weighs 513 g gross and its excluded packaging weighs 12 g. The calculated food weight is 501 g. Comparing the 513 g gross reading directly with a 500 g food declaration would incorrectly credit packaging as product.
As a practical method, write a tare specification for each packaging configuration. Include the bag, closure, label, tray, board, liner, sleeve, or other excluded components actually present during weighing. A promotional sleeve or replacement tray can change gross weight without changing food quantity. Specify the condition of packaging used for the tare determination rather than recording only a single unexplained number.
Representativeness matters as much as arithmetic. Packaging can vary between supplier batches, formats, and individual units. If the actual tare were 14 g but the calculation deducted 12 g, the reported net weight would be 2 g too high. If actual tare were 10 g, the same deduction would understate net weight by 2 g. Either direction can distort operational decisions.
Handbook 133’s tare procedures explicitly address packaging variability and different tare methods. For production practice, compare the selected tare basis with packaging from the relevant run and investigate meaningful variation. Do not assume that weighing unused packaging is interchangeable with the applicable official inspection method. Food clinging to a wrapper, absorbed moisture, cleaning, and drying can affect the comparison and need a defined treatment.
Record the gross reading, tare value or tare-study reference, calculated net weight, units, and package identity. Where an average tare is used, describe the result as net weight calculated using that average, not an individually established packaging weight. Reassess the basis after packaging changes or unexplained shifts. Preserve earlier calculations and document corrections, including their effect on decisions already made; silently replacing yesterday’s tare hides the original evidence.
4. Define when the weight matters
A bakery weight has a time and condition attached to it. Dough-piece weight, oven-exit weight, cooled product weight, wrapped weight, and weight after distribution are not interchangeable. As production practice, define the measurement stage precisely: for example, after the established cooling process, after slicing, and with the complete retail packaging present. Record departures from those conditions rather than treating all readings as comparable.
Theoretical bake yield estimates the relationship between an upstream input and a later output under assumed conditions. It does not measure the net contents of an individual retail pack. A favorable batch yield can coexist with variable loaf weights, missing pieces, uneven topping, or packaging errors. Use yield analysis to investigate the process, while retaining finished-pack measurement as its own control.
For a practical cooling study, identify matched products and record weights at defined stages, elapsed times, packaging condition, and relevant storage conditions. Keep handling consistent and account for sampling losses such as crumbs removed during opening. Separate loss before wrapping from changes after packaging. The resulting observations apply to the studied product, package, and conditions; they should not automatically be transferred to another bread or pastry.
The distribution boundary also matters. Handbook 133 explains why point-of-pack inspection cannot entirely replace wholesale or retail testing, including distribution effects and moisture loss. FDA’s recognition of reasonable moisture variation in 101.7(q) is scoped to good distribution practice. Do not borrow a moisture allowance for another commodity or invent a universal bread percentage. Handbook guidance directs inspectors to their jurisdiction when no predetermined allowance exists.
Use measured cooling and storage behavior when reviewing the site target, but do not reduce necessary baking or cooling merely to retain weight. Food safety, product quality, shelf life, and net quantity need compatible controls. Align bakery production planning with the required process stages so that pressure to pack quickly does not turn a warm measurement into an unsupported prediction about later net contents.
5. Verify actual weighing readiness and reject operation
Production practice starts with readiness, not the presence of a calibration sticker. Confirm the instrument identity, suitable capacity, package support, selected units, zero condition, and operating environment. Check for vibration, drafts, product contact with surrounding surfaces, debris, and unstable indications. Follow the equipment instructions and the site’s approved measurement procedure. A previous satisfactory result does not resolve an abnormal reading today.
Resolution is the displayed increment; accuracy concerns agreement with the reference value. A fine display can still be biased, unstable, or unsuitable for the decision. Evaluate performance around the actual gross and tare loads, using appropriate reference standards and a documented acceptance basis. Practical suitability for detecting a process shift is separate from satisfying the equipment provisions of an official inspection procedure.
Handbook 133 separates measurement equipment checks from package testing. Its equipment procedures should not be reduced to a claim that one display increment makes every scale acceptable. For production use, establish verification and calibration arrangements from applicable requirements, manufacturer instructions, usage, environment, and performance history. This guide does not prescribe a universal calibration interval or substitute a readiness check for calibration.
Where an in-motion checkweigher is used, independently check its product setup against the approved package specification. Compare identified packs with a suitable reference weighing method under controlled timing and packaging conditions. Examine whether the configured quantity is gross or calculated net, which tare is applied, and which thresholds are active. A correct product name on the screen does not prove that every underlying setting is correct.
Confirm the physical result of a reject challenge using controlled, identifiable test packs and a safe procedure. Observe that the intended pack leaves the accepted stream and reaches the designated controlled location; an alarm or displayed reject count alone is insufficient evidence. Keep test packs out of saleable stock. If measurement or removal fails, use the site’s stop, containment, investigation, and recheck process before relying on the system again.
6. Design sampling around the production decision
A production sampling plan should state what it is intended to detect and which output it represents. As practice, cover relevant lanes, portioning heads, time periods, restarts, and packaging changes rather than taking only convenient packs from one location. Select the number and timing of checks according to variability, production rate, detection needs, and the consequence of delayed discovery—not a universal sample count.
Keep routine monitoring separate from targeted investigation. Packs chosen because they look unusually small can help diagnose a problem, but they do not form an unbiased estimate of ordinary output. Preserve the selection method with the results. Handbook 133 distinguishes audit checks from its structured inspection plans; a bakery’s routine sample does not automatically become an official lot inspection.
- 1. Define setupIdentify the product, declaration, package revision, timing, and site target.
- Approved specification
- 2. Check readinessVerify weighing setup and, where used, physical reject operation. Failure → step 5.
- Check results
- 3. Collect samplesSelect across the planned production conditions; record gross, tare, net, and time.
- Selection method
- 4. Review findingsAssess individual readings, average, spread, and trend. Concern → step 5; otherwise continue planned monitoring.
- Site action criteria
- 5. Contain and investigateIdentify suspect output and prevent unintended dispatch while the cause is assessed.
- Hold boundary
- 6. Correct and recheckDocument changes and new evidence. Unresolved result → step 5.
- Original data retained
- 7. Human disposition reviewAuthorize release, rework, or other disposition for identified stock; resume approved monitoring.
- Decision and rationale
Review the average alongside individual values and their sequence. A stable mean can conceal an erratic portioner, while an overall shift may reflect tare or instrument setup rather than food quantity. Repeated measurements of the same pack help investigate measurement behavior, but are not additional independent production packs. Retain that distinction when calculating sample size and describing coverage.
7. Worked fictional example: twelve 500 g packs
The following fictional example is a nonlegal production illustration. Twelve packs have a nominal net declaration of 500 g. Assume their net weights have been determined on a consistent, verified measurement basis at the same defined cooling and packaging stage. Twelve is chosen to make the arithmetic visible; it is not a mandated sample size or a proposed inspection plan.
The table shows net measurements, not gross weights. The difference column is measured net weight minus 500 g: negative values identify shortfalls against that reference, positive values identify excess, and zero means equality at the recorded measurement resolution. Grams are used for calculation; this is not a complete US retail-label template.
| Pack | Measured net weight, g | Difference from 500 g, g |
|---|---|---|
| 1 | 496 | −4 |
| 2 | 498 | −2 |
| 3 | 500 | 0 |
| 4 | 501 | +1 |
| 5 | 502 | +2 |
| 6 | 499 | −1 |
| 7 | 503 | +3 |
| 8 | 504 | +4 |
| 9 | 500 | 0 |
| 10 | 497 | −3 |
| 11 | 505 | +5 |
| 12 | 501 | +1 |
The total measured net weight is 6,006 g. Dividing by 12 gives a sample mean of 500.5 g. The minimum is 496 g, the maximum is 505 g, and the range is 505 − 496 = 9 g. Four packs are below 500 g: packs 1, 2, 6, and 10. Six are above it, and two equal it.
These calculations describe only the twelve observations. They do not establish the population mean, the frequency of low packs throughout the run, or legal acceptance of an inspection lot. No MAV comparison is made. The four low readings are reasons to examine the process and applicable site rules, not grounds for declaring four legal violations from this table alone.
Before adjusting the line, ask where these packs came from. Consecutive packs from one lane tell a different story from packs spread across a run. Preserve lane and time information so the light values can be investigated without assuming that the displayed sequence proves a production trend.
8. Reconcile excess without hiding shortfalls
An aggregate excess figure is useful only when its definition is clear. In the fictional sample, the nominal total is 12 × 500 = 6,000 g, while the measured total is 6,006 g. The signed difference is therefore +6 g. Calling that value simply ‘giveaway’ would hide the coexistence of excess in some packs and shortfalls in others.
| Sample measure | Calculation | Result and meaning |
|---|---|---|
| Total shortfall magnitude | 4 + 2 + 1 + 3 | 10 g below the reference, across four packs |
| Positive excess only | 1 + 2 + 3 + 4 + 5 + 1 | 16 g above the reference, across six packs |
| Signed net excess | 16 − 10 | +6 g relative to the nominal sample total |
| Mean signed difference | 6 ÷ 12 | +0.5 g per sampled pack |
| Nominal reconciliation | 6,000 + 16 − 10 | 6,006 g measured total |
Positive excess and signed net excess answer different questions. The first measures food above the reference in the above-reference packs. The second measures the sample’s total difference after shortfalls offset excess mathematically. That offset does not move food between packages, remedy a deficient pack, or resolve the individual-package part of an applicable inspection. Report both quantities when discussing material use.
For a fictional sample-only valuation, assume a uniform incremental food-material cost of $4 per kilogram at the measured finished-product state. The 16 g positive excess corresponds to 0.016 × $4 = $0.064. The signed 6 g difference corresponds to 0.006 × $4 = $0.024. Neither figure is demonstrated avoidable savings, and the 10 g shortfall is not a legitimate cost-saving opportunity.
Do not multiply this small sample into a daily savings promise. A projection would need justified assumptions about representativeness, stable output, run volume, product cost, moisture state, and the consequences of changing the target. Some excess may be deliberate operating margin. Evaluate rejected product, rework, packaging consumption, and labor separately rather than treating every gram above nominal as recoverable material.
9. Adjust the cause, then review affected stock
A practical response plan distinguishes a change in average from a change in spread, a measurement problem, and a later moisture change. Do not make every low reading trigger an immediate increase in the portioner setting. First establish that the package identity, tare, timing, and weighing method are correct. Otherwise, the adjustment may compensate for a false signal and create a new problem.
| Observed pattern | Investigate first | Practical response |
|---|---|---|
| Average moves downward; spread remains similar | Portioner setting, material feed, process stage | Confirm the shift; adjust under approved rules and assess earlier output |
| Spread increases without much mean change | Uneven portions, lanes, topping, measurement instability | Address the variation rather than only raising the target |
| Gross rises after a packaging change | New tare and package configuration | Re-establish the net-weight basis before changing food quantity |
| Reference scale and checkweigher disagree | Timing, units, tare, motion, setup | Resolve measurement disagreement and contain suspect output |
| Later weights fall relative to packing weights | Cooling completion, packaging, storage conditions | Study the loss and review the relevant target and distribution assumptions |
Raising a target can provide more operating margin, but may increase food use, package fit problems, and rework. Lowering it may reduce positive excess while increasing exposure to low packs. Reducing process variation can be more useful than repeatedly moving the mean. These are trade-offs to test with production evidence, not guaranteed outcomes or permission to run below applicable requirements.
Define a provisional suspect interval using the last trustworthy evidence, known process changes, stoppages, and the discovery time. A satisfactory sample at an earlier time does not prove every intervening pack was satisfactory. Identify affected stock physically and in records, then decide what additional examination is needed. Keep already rejected packs under control while that assessment proceeds.
Record the adjustment time and setting separately from the hold decision. A successful later recheck supports the corrected process; it does not erase earlier weights or release earlier stock. An authorized person should review the original findings, containment scope, recheck evidence, and proposed disposition before releasing identified packages or approving rework.
10. Link each result to the evidence behind it
Useful records let a reviewer reconstruct what was measured and why a decision was made. As a practice, organize results around identified sampling events rather than a spreadsheet of anonymous weights. A result should lead back to the production run, package revision, weighing device and checks, tare basis, and measurement time. This is a record-design recommendation, not a claim about any software product.
Production Run
One run → many sample events; retain the boundaries of the output represented.
- run_id
- lot_code
- line and production interval
Package specification
One revision → many events; a changed configuration needs an identifiable revision.
- package_revision
- declaration
- components and site target
Sample event
References the other evidence records; contains individual pack measurements.
- event_id and referenced IDs
- pack IDs, gross, tare, net, units
- weighed_at, cooling stage, selection method
Scale Evidence
Links the device and relevant checks to events that relied on them.
- device_id
- check time, reference, results
Tare Study
Supports the tare applied to a defined packaging population and period.
- tare_study_id
- method, observations, variability
Disposition Review
Covers identified events and stock; retains original findings and later rechecks.
- hold scope
- adjustment and recheck references
- reviewer, time, decision, rationale
The production lot and the official inspection lot are not necessarily identical. Handbook 133 states that the official defines the inspection lot, which may be smaller or larger than the packer’s production lot. Keep internal run boundaries precise without assuming they dictate an inspector’s scope. Lot genealogy provides related context for connecting packaged output with its production history.
Preserve original readings, corrections, invalidated measurements with reasons, and recheck results as distinguishable records. If a tare error is discovered later, show which events used it and what was reassessed. Missing measurements should remain visible rather than becoming zeros. These distinctions make review possible without confusing a corrected calculation, a repeated measurement, and a newly sampled package.
11. Implement a usable control plan
Begin with one product family and its actual packaging configurations. As a practical implementation approach, walk the route from cooling through wrapping, weighing, case packing, storage, and dispatch. Identify where meaningful measurements can be made and where suspect stock can be controlled. Agree on responsibilities before selecting a reporting tool: the essential system is the measurement-and-decision process, not the screen displaying it.
- Approve the declared quantity reference, package components, measurement stage, and separate site target for each configuration.
- Establish a representative tare basis, with a method for recognizing packaging changes and assessing variability.
- Document equipment suitability, readiness checks, abnormal-performance responses, and independent checkweigher comparisons where applicable.
- Specify production sampling coverage, selection methods, review criteria, and escalation triggers without presenting them as statutory sample sizes.
- Test physical reject removal where used, and define who controls rejected packs and challenge materials.
- Define hold identification, suspect-period assessment, recheck methods, and authorization for release or rework.
- Retain original results and connect adjustments, corrected calculations, and disposition decisions to the affected output.
- Train operators using both normal examples and failures, including wrong tare, missed sampling, and unsuccessful rejection.
Run a controlled trial of the plan. Ask another trained person to reconstruct a sample calculation and locate the stock covered by a simulated hold. Check whether shift handovers communicate unresolved findings and whether a package change reaches everyone using the tare value. Revise unclear instructions before extending the approach to other lines. Review the plan when evidence shows that its coverage or response is inadequate.
When evaluating food traceability software or other record tools, ask neutral questions: Can the proposed setup preserve original readings and revisions? How are missing or duplicated readings identified? Can a reviewer retrieve the applicable tare and device-check evidence? What happens during downtime? Require a demonstration against your workflow rather than assuming that integration or a dashboard supplies these controls.
Keep improvement reviews focused on measured variation, unexplained changes, containment effectiveness, and decision quality. A useful program supports timely action while keeping legal inspection, equipment verification, and production optimization clearly separated.
Questions
Must every bakery package be weighed?
Do not assume a universal requirement to weigh every pack from the provisions discussed here. Choose production monitoring coverage through the bakery’s applicable requirements and process assessment. Checking every pack may provide more observations, but it still depends on correct tare, valid measurement, reliable removal where used, and handling of downtime or bypassed output. Sampling can support process monitoring when its coverage matches the decision. Neither approach automatically establishes legal lot acceptance. Handbook 133 uses defined inspection sampling procedures; an operational line record is not interchangeable with that inspection merely because it contains many weights.
Does a 500.5 g sample mean prove that a 500 g lot passes?
No. In the fictional example, 500.5 g is the average of twelve observed packs, not proof about every package or the complete production lot. A legal assessment depends on the applicable inspection lot, sampling method, measurement procedure, and acceptance criteria, including the individual-package assessment. Operationally, the mean also needs context: which lanes and times were represented, whether tare was sound, and whether cooling conditions were consistent. Retain the individual readings and investigate relevant patterns. Do not replace those observations with a single favorable average or treat the example as a release authorization.
Is every pack below its declaration a legal violation?
A below-declaration measurement is a negative difference, but it is not automatically an MAV violation. FDA 101.7(q) recognizes specified reasonable variations while prohibiting unreasonably large variations. Handbook 133 distinguishes average and individual-package assessments and applies the relevant inspection procedures. A bakery may establish internal triggers that prompt action before an official inspection boundary would be reached. Label those triggers as site controls, not legal tolerances. Check measurement validity, follow the internal response plan, and obtain the applicable regulatory assessment rather than declaring compliance or noncompliance from one unexplained display reading.
Can one tare value be used for all bakery packs?
As production practice, use a tare basis that represents the actual package configuration and the population to which it is applied. One value should not be carried across bags, trays, boards, closures, and promotional packaging without justification. Even nominally identical materials can vary. Record how the value was established, which materials it covers, and what changes trigger reassessment. If an average tare is applied, retain the study behind it and understand its effect on individual calculated net weights. For official inspection, follow the applicable tare procedure rather than assuming the production method is equivalent.
How much extra weight should the site target include?
There is no universal extra-weight setting supplied by this guide. Develop the target from the declared quantity, observed process variation, measurement performance, product timing, relevant distribution behavior, and applicable requirements. An MAV is not a recommended short-fill target, and a favorable sample mean does not demonstrate enough operating margin. As practice, test proposed changes under controlled conditions and examine individual results, spread, rejects, and material use. Improve unstable portioning or measurement before relying on a higher target to conceal it. Document the reasoning and reassess the target when products, packaging, or process conditions change.
Can cooling loss justify a lighter finished package?
Do not treat cooling loss as an automatic exemption. Loss before packaging, changes after packaging, and theoretical baking yield are different matters. FDA 101.7(q) recognizes reasonable moisture variations during good distribution practice, but that is not a blanket allowance for underfilling at manufacture. Handbook 133 directs inspectors to jurisdictional guidance when no predetermined moisture allowance exists. As production practice, study matched products under defined timing, packaging, and storage conditions. Use those observations to review targets and investigate shortages, without borrowing another commodity’s allowance or changing necessary baking and cooling solely to retain weight.
Why is the sample’s 6 g net excess not the same as giveaway?
The signed 6 g excess subtracts 10 g of shortfalls from 16 g of positive excess. It describes the total sample relative to twelve nominal 500 g packs, but it conceals how quantity is distributed among packages. The 16 g figure describes excess in the six above-reference packs; neither figure alone establishes avoidable material use. Some operating margin may be intentional, and adjustments may affect rejects or rework. Any valuation needs an explicit cost basis, while any projection needs representative data and stable-process assumptions. Shortfalls must not be counted as an acceptable saving.
What should happen after an adjustment produces satisfactory rechecks?
Separate permission to continue the corrected process from disposition of previously produced stock. As practice, retain the original results, document the adjustment and recheck conditions, and identify the output covered by each finding. Review whether earlier packs require further examination, rework, or another controlled disposition. A later satisfactory reading does not erase a failed reject challenge, an incorrect tare, or low weights recorded earlier. An authorized person should review the evidence and record the decision for identified stock. Keep unresolved holds visible across shifts and prevent affected packages from entering normal dispatch by mistake.
Sources
Practical orientation, not legal advice. Rules differ by jurisdiction; your quality and compliance team decides what applies.