Foreign material control: hazard decisions, checks and disposition
A passed metal-detector check does not close a torn-screen investigation.
In Short
- This guide addresses FDA human-food operations under 21 CFR Part 117.
- For an operation subject to §117.130, the written hazard analysis must identify and evaluate known or reasonably foreseeable hazards for each food type, including…
- Walk the product path from bag opening to the final closure.
The plant still needs to establish which product was exposed, what the remaining controls could remove, and who can authorize disposition. Start with the physical hazard—not the equipment purchase.
Establish which requirements apply
This guide addresses FDA human-food operations under 21 CFR Part 117. Its operating principles can inform food-processing, bakery and meat-sector teams, but it does not state USDA, drug, dietary-supplement or animal-food requirements.
Before applying the Subpart C duties below, document applicability for the facility and activity. Identify any exemption being relied on, its conditions, and the requirements that remain applicable. Section 117.3 recognizes a qualified-facility exemption by reference to §117.5(a); this guide does not determine eligibility. Establish Subpart G applicability separately rather than assuming that every ingredient or receiving operation has the same supply-chain duties.
Under §117.5(a), qualified facilities are exempt from Subparts C and G, subject to withdrawal under Subpart E, and must follow the modified requirements in §117.201. They must attest to FDA to qualified-facility status and either hazard identification, preventive controls and monitoring, or compliance with applicable non-Federal food safety law, and retain supporting records. Status must be determined and documented annually by July 1; after the initial submission, attestations are submitted every two years during October 1–December 31. Where §117.201(e) applies, consumers must receive the manufacturing or processing facility’s name and complete business address on the required label or through the specified point-of-purchase notification. This is not a blanket Part 117 waiver or an eligibility determination. The worked scenario assumes Subparts C and G apply.
Decide whether the physical hazard requires a preventive control
For an operation subject to §117.130, the written hazard analysis must identify and evaluate known or reasonably foreseeable hazards for each food type, including physical hazards such as stones, glass and metal fragments. The evaluation considers injury severity and the probability of occurrence in the absence of preventive controls, together with equipment, ingredients, processing, packaging, intended use and the intended consumer. The analysis must be written even when it identifies no hazard requiring a preventive control.
Foreign material is not automatically a hazard requiring a preventive control. Section 117.3 defines a hazard by its potential to cause illness or injury; the further decision to establish a preventive control follows the hazard analysis. A soft liner fragment, a sharp wire and a stone should not receive an identical assessment merely because all are foreign material. Document the material, plausible fragment characteristics, route into food, exposure and injury potential.
A conclusion that a particular physical hazard does not require a preventive control needs a defensible written rationale. Do not reason that metal is unlikely simply because a detector will remove it: the probability assessment is made in the absence of preventive controls. Nor does a no-preventive-control conclusion remove applicable contamination obligations. Section 117.80(c)(8) requires adequate measures against metal or other extraneous material; §117.40(a)(2) addresses equipment design, construction and use to avoid contamination, including metal fragments.
Where a hazard requires a preventive control, §117.135 requires written controls that significantly minimize or prevent it. Those controls can be at a critical control point or elsewhere. The provision sets a control outcome; it does not prescribe a metal detector for every line. The site must select the control, establish relevant parameters and support its capability for the actual food and process.
Map where fragments can enter the powder stream
Walk the product path from bag opening to the final closure. Record both the source and its position relative to the last effective control. An ingredient sifter cannot address a fragment introduced later by a blender, transfer screw or packer.
| Source | Credible route into food | Site investigation and prevention focus |
|---|---|---|
| Bags and liners | Cut bag corners, paper fibers, film strips or a liner drawn into the dump station | Observe opening and emptying; control cutting and loose packaging; inspect the dump station and retained material. |
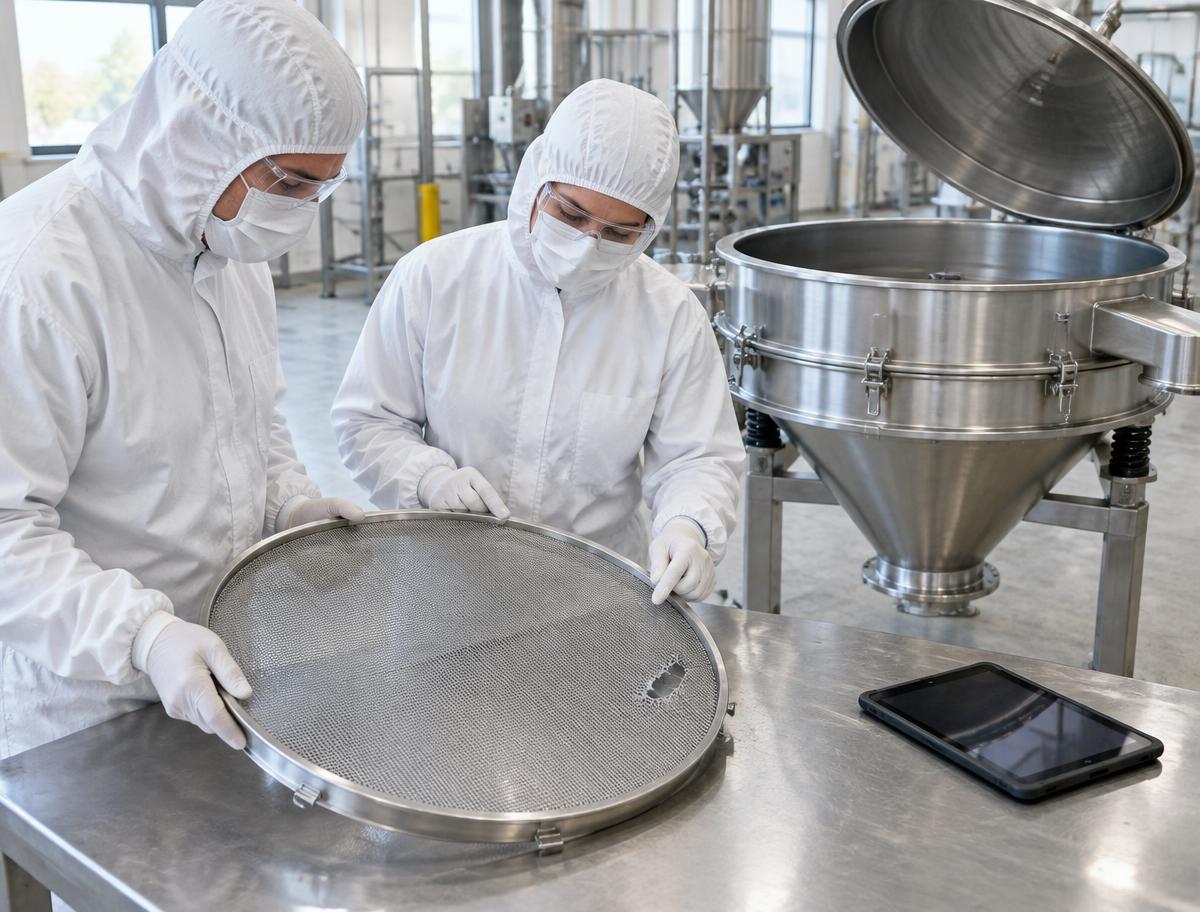
| Sieve or sifter screen | Broken wires, torn mesh, damaged seals or product bypass around the screen | Inspect mesh, perimeter, supports and seals; identify screen material; retain the failed assembly for examination. |
| Magnet assembly or loss of capture | Damaged housing or mounting, poor seating, accumulated material, or inadequate contact with the product stream | Check physical integrity, installation and cleaning; assess capture performance separately from a visual inspection. |
| Totes, knives and tools | Chipped tote edges, blade tips, scraper pieces, fasteners or repair debris | Inspect containers and tools; control tool condition and repairs; account for damaged components before restart. |
| Wear metal | Abrasion or contact at screws, bearings, blender internals, valves and conveyors | Inspect likely contact points; compare recovered material with equipment; investigate changing quantities or fragment types. |
These are investigation prompts, not a universal list of hazards requiring preventive controls. Add sector-specific sources to the same map. Bakery handling may introduce material after flour sifting; another FDA-covered food process may add inclusions or use different packaging after its main separation step.
Layer controls without giving any layer credit it has not earned
| Control | Useful role | Important limit | Evidence to establish at the site |
|---|---|---|---|
| Sieves and sifters | Separate material that cannot pass through the selected intact screen under operating conditions | Thin, flexible or elongated fragments may pass or orient through an opening. Damage and bypass defeat separation; the screen can itself shed material. | Screen specification and condition; sealing and bypass control; performance with the relevant fragment geometry, product and flow. |
| Magnets | Capture magnetically responsive metal when the stream makes effective contact with the assembly | Do not assume capture of every alloy or stainless fragment. Non-metal hazards remain. Loading, placement, flow and assembly damage can impair performance. | Relevant material response; installation and product contact; cleaning and inspection method; suitable performance assessment. |
| Metal detection | Identify responsive metal in a defined product and package configuration and trigger removal or a controlled stop | Does not detect paper, plastic, glass or stone as such. Metal type, shape, orientation, product, package and installation affect performance. Detection alone does not prove successful rejection. | Representative challenges under operating conditions; approved settings; actual diversion or stop response; control of rejected product. |
| X-ray inspection | Identify some foreign material with sufficient contrast against the product and package | Not a universal foreign-material detector. Low-density plastics, thin material and poorly contrasted objects may escape detection; presentation and overlap matter. | Capability for the target objects in the actual pack and product; representative presentation; verified rejection or stop response. |
Choose the sequence from the hazard locations. An upstream separator can reduce incoming contamination while a downstream inspection step addresses later introduction. Several devices with overlapping blind spots do not necessarily provide effective control. No numeric sensitivity, screen aperture or magnet-strength target in this guide is a regulatory specification.
For applicable preventive controls, §117.160 requires validation as appropriate to the control and its role. Validation includes scientific and technical evidence—or studies when that evidence is unavailable or inadequate—and must be performed or overseen by a PCQI. The section permits a PCQI-prepared or overseen written justification that validation is not applicable for certain other preventive controls. Do not treat a supplier brochure or a routine successful challenge as proof of capability for every possible contaminant.
Use CPG 555.425 as enforcement policy, not a design specification
FDA CPG Sec. 555.425 addresses hard or sharp foreign objects. Its direct-reference seizure and import-detention criteria combine two conditions: the product contains a hard or sharp foreign object measuring 7 mm to 25 mm in length, and the product is ready-to-eat or requires only minimal preparation that would not eliminate, invalidate or neutralize the hazard before consumption. The CPG gives heating as an example of such minimal preparation.
The background states that objects less than 7 mm in maximum dimension rarely cause trauma or serious injury except in special risk groups, including infants, surgery patients and the elderly. That is not a declaration that smaller objects are safe.
- For a 7–25 mm object where additional preparation or processing may affect its presence in the finished food, the CPG calls for that processing to be described in the recommendation for legal action. It specifically notes that sifting may or may not remove an object, depending on its measurements and the mesh aperture.
- Objects less than 7 mm in length where a special-risk group is among the intended consumers, and objects over 25 mm in length, are also addressed through recommendations for legal action and CFSAN health-hazard review.
- For those additional-review categories, the CPG describes adulteration under 21 U.S.C. 342(a)(1) if CFSAN review establishes a health hazard. It also provides a separate unfit-for-food consideration for certain cases where no health hazard is found.
Separate operating checks, verification and the records that support them
Section 117.3 defines monitoring as a planned sequence of observations or measurements assessing whether controls operate as intended. Verification goes beyond monitoring to evaluate operation and the validity of the food safety plan. Label the activity by its purpose in the plan—not simply because the form is called a verification sheet.
| Activity | Applicable requirement | What the site must resolve |
|---|---|---|
| Operating checks | Subpart C implementation records include monitoring of preventive controls (§117.190). | Define the observation or challenge, responsible role, acceptance criteria and schedule. Record actual results, including failed and missed checks. |
| Instrument calibration or accuracy checks | Section 117.165 includes calibration of process-monitoring and verification instruments, or checking their accuracy, as appropriate. Written procedures address method and frequency. | Identify the instruments involved and suitable methods. A detector challenge is not automatically equivalent to every needed accuracy or calibration activity. |
| Monitoring and corrective-action record review | Under §117.165, review is by or under PCQI oversight within 7 working days after the records are created, or a reasonable longer timeframe supported by a PCQI-prepared or overseen written justification. | Assign the reviewer and escalation route. Do not wait for the review deadline to contain product after a known failure. |
| Other verification record review | Calibration, testing and other verification records are reviewed by or under the oversight of a PCQI within a reasonable time after the records are created under §117.165. | Set a usable review interval and investigate trends, missing evidence and unresolved decisions. |
| Capability evidence | Validation requirements and exceptions are addressed in §117.160. | Show that the control can address the identified hazard under relevant conditions; distinguish capability evidence from routine evidence that the equipment operated. |
Set check frequency around the failure modes and the amount of product the site can reliably contain. Consider startup, changeover, interventions, operating checks and end-of-run checks when designing the schedule. These are site decisions, not a universal interval supplied by the cited provisions. A long interval can create a large uncertain product window.
A useful detector-check record identifies the line, product, package, approved configuration, test pieces, challenge method, time, operator, detection result and reject or stop response. Where installed, include the relevant reject-bin, confirmation and interlock checks. A challenge that alarms but fails to remove the test product is not a successful end-to-end check.
For a sifter, record the screen identity, inspection coverage, mesh and perimeter condition, seals, bypass observations and retained material. For a magnet, distinguish a condition and cleaning inspection from evidence of capture capability. Use explicit pass, fail and not-established results; a blank field is not a pass.
Section 117.190 requires applicable food-safety-plan implementation records for monitoring, corrective actions and verification, including validation, calibration and records review where applicable. These records are subject to Subpart F. A standalone tool register, maintenance photo file or foreign-material trend chart is not named as a universal Subpart C form. Such operational records may be optional additions, but evidence used to document a required activity is not optional merely because it sits in a maintenance system.
Contain rejects, investigate the failure and decide the food’s disposition
Treat a production reject and a failed control check as different events. A reject may show that a functioning control removed suspect product; a failed challenge or damaged screen calls the control’s performance into question. Secure rejected material, identify its product and time window, and investigate it without returning it to production by default. A second pass with no alarm does not explain the first reject.
- 1. Preserve the evidenceStop or isolate the affected stream as appropriate. Secure rejects, failed parts, settings and relevant records.
- 2. Bound the uncertain intervalStart with the last reliable good check and the product actually exposed. Expand the scope if inspection quality, carryover or timing is uncertain.
- 3. Reconcile and holdLocate affected lots, work-in-process and rejects. Reconcile quantities and prevent release while safety is unresolved.
- 4. Evaluate control and foodIdentify the fragment and failure mechanism. Assess downstream capability, corrective action and any proposed reconditioning method.
- 5. Record the decisionThe authorized site decision-maker releases only with an adequate safety basis, approves appropriate reconditioning or disposal, or keeps the material held when evidence remains unknown.
An end-of-shift torn-screen finding means the failure time is unknown unless other evidence establishes it. The investigation therefore asks what passed through since the last demonstrably good inspection—not just what was running when the tear was discovered. An inadequate earlier check, mixed downstream inventory or retained material can require a wider scope. A clean magnet or a quiet detector log narrows the investigation only to the extent that its capability and operating evidence support that conclusion.
Where §117.150 applies, corrective-action procedures must address identifying and correcting the problem, reducing recurrence when necessary, evaluating all affected food for safety, and preventing affected food from entering commerce if its non-adulterated status cannot be ensured. Corrective actions, and corrections when appropriate, must be documented. An unanticipated ineffective control can also require reanalysis of the food safety plan when appropriate. The exception for a timely correction of a minor, isolated problem does not fit a screen failure with unresolved product-safety implications.
What supports product evaluation?
- Characterize recovered material: composition, hardness, sharpness, dimensions, shape and likely source. Preserve the failed part and compare it with recovered pieces; one matching wire does not account for all missing material.
- Establish exposure: check times and reliability, equipment location, product movement, carryover and all affected inventory. Record uncertainty instead of assigning a convenient failure time.
- Assess remaining controls: determine whether they were capable of controlling this material in its possible shapes and orientations, and whether records show effective operation during the affected interval.
- Evaluate a proposed reconditioning method for this contamination. A clean sample or a successful rerun is not, by itself, evidence that sparse fragments have been removed from the entire lot.
- Separate the food decision from the repair decision. Record the disposition basis, quantity, authorizing role and any unresolved evidence. Assign PCQI involvement where the applicable validation and review provisions require it.
Section 117.80(a)(6) requires food contaminated to the point of adulteration to be rejected or, if appropriate, treated or processed to eliminate contamination. Section 117.80(c)(9) addresses protective disposal and, where adulterated food can be reconditioned, either an appropriate method proven effective or appropriate reconditioning followed by reexamination and a finding that the food is not adulterated before incorporation into other food. Rescreening is therefore a method to evaluate—not an automatic release authorization.
Worked example: a torn discharge-sifter screen
Fictional scenario: the times, quantities, checks and role assignments below are site assumptions, not regulatory limits. A dry-mix line runs from bag dumping to blending, discharge sifting, a magnet, packaging and final metal detection. Its food safety plan identifies sharp screen wire as a hazard requiring a preventive control. The product requires cooking, but the site has no basis to claim that cooking removes wire.
At 12:00, a documented empty-line inspection finds the discharge screen, perimeter and seals intact. Three lots then pass through the line. At the 16:00 end-of-shift inspection, the operator finds torn mesh and missing wire. No evidence establishes when the damage began. The site includes every lot produced after the 12:00 check in the affected population.
| Time or interval | Record or observation | Result | Consequence |
|---|---|---|---|
| 12:00 | Empty-line screen and seal inspection; downstream line clearance recorded | Last reliable good inspection | Defines the starting boundary under these scenario assumptions. |
| 12:00–13:20 | DM-201 production record | 1,000 kg; no detector production rejects | Include all 1,000 kg. |
| 13:20–14:40 | DM-202 production and reject records | 1,000 kg including one 5 kg detector reject | Include the reject within the lot total, not in addition to it. |
| 14:40–16:00 | DM-203 production and reject records | 1,000 kg including one 5 kg detector reject | Include the reject within the lot total. |
| 12:00, 14:00 and 16:00 | Detector challenge log | Configured challenges detected and actually rejected | Passes establish only the tested performance; capability for missing screen-wire geometries remains unestablished. |
| 16:00 | End-of-shift screen inspection | Fail: torn mesh and missing wire | Stop the line; preserve the screen; contain the full 3,000 kg population. |
| 16:05 | Magnet inspection | Assembly intact and seated; no visible wire recovered | Does not establish capture of the missing wire. Screen-alloy response is still unknown. |
| Following morning | Controlled trial on a separate intact sifter | 1,995 kg processed; 5 kg of retained product and debris isolated; one wire recovered | Trial completion is not release approval. Missing-fragment accounting and method capability remain unresolved. |
The initial containment is 2,990 kg in the main product hold plus 10 kg already secured as detector rejects. The trial uses all 1,000 kg of DM-201 and the 995 kg non-rejected portion of DM-202. It retains 2 kg from DM-201 and 3 kg from DM-202, including the recovered wire and associated product. For this scenario, weights reconcile with no other withdrawals or losses.
| Lot | Affected kg | Trial rescreen input kg | Rescreened output still held kg | Unprocessed held kg | Segregated rejects kg | Released kg |
|---|---|---|---|---|---|---|
| DM-201 | 1,000 | 1,000 | 998 | 0 | 2 | 0 |
| DM-202 | 1,000 | 995 | 992 | 0 | 8 | 0 |
| DM-203 | 1,000 | 0 | 0 | 995 | 5 | 0 |
| Total | 3,000 | 1,995 | 1,990 | 995 | 15 | 0 |
The final inventory balance is 3,000 kg = 1,990 kg rescreened and held + 995 kg unprocessed and held + 15 kg segregated rejects + 0 kg released. The 15 kg comprises the original 10 kg detector rejects and 5 kg trial retains. Rescreen input is an activity total, not another inventory category. All 3,000 kg remain contained: 2,985 kg in product hold and 15 kg in reject storage, with no destruction or shipment yet recorded.
Screen replacement, installation checks and restart acceptance are tracked separately. The corrective-action record also asks whether the inspection method and interval should change, whether similar screens need examination, and whether the food safety plan needs reanalysis. Closing the maintenance work order does not close the food disposition.
Questions
Does every FDA human-food line need a metal detector?
The cited Part 117 provisions require adequate protection against extraneous material and, where applicable, written controls for hazards requiring a preventive control. They do not name a metal detector as the required device for every line. Select equipment from the hazard analysis and demonstrate that the chosen control or combination can address the relevant material. A detector cannot substitute for controls on non-metal hazards or contamination introduced after inspection.
Can a physical hazard be evaluated without becoming a preventive control?
Yes. Section 117.130 requires identification and evaluation, not an automatic preventive-control designation for every possible fragment. The written analysis must assess injury severity and probability in the absence of preventive controls. Document why a particular hazard does or does not require a preventive control, while maintaining applicable contamination protections. Do not base a no-control conclusion on the assumed success of the very detector being evaluated.
Does FDA’s 7–25 mm policy permit smaller fragments?
No. CPG 555.425 describes enforcement criteria for hard or sharp foreign objects, not a permitted contamination range. The direct-reference criteria combine 7–25 mm in length with ready-to-eat food or only minimal preparation that would not neutralize the hazard. The CPG also addresses smaller objects for special-risk consumers and objects over 25 mm. Its background specifically identifies infants, surgery patients and the elderly as special risk groups.
How often should screens, magnets and detectors be checked?
Establish a documented site schedule from the control’s failure modes, product exposure and ability to contain the affected interval. Startup, changeovers, interventions and end-of-run checks are useful points to assess, not a universal mandatory schedule. Keep operating checks distinct from instrument calibration or accuracy checks. Section 117.165 requires appropriate written calibration or accuracy-check procedures addressing method and frequency; it also sets record-review requirements.
What if the last good screen check is missing or unreliable?
Do not invent a failure time or limit the hold to the current lot. Identify the earliest reliable evidence of acceptable condition and assess all potentially exposed product, including downstream carryover. Expand the containment boundary when that evidence cannot support a narrower one. Record the uncertainty and keep disposition open until the safety evaluation provides an adequate basis.
Can a detector reject be released after passing a second time?
Not on that result alone. A repeat pass does not establish why the original rejection occurred or exclude an intermittent response, fragment orientation effect or reject-system issue. Keep the material controlled, investigate the original event and apply the site’s product-evaluation procedure. Where §117.150 applies, affected food must be evaluated and kept out of commerce if its non-adulterated status cannot be ensured.
Does rescreening automatically make a torn-screen lot acceptable?
No. Evaluate whether the proposed method can remove the actual fragments, including thin wire that may orient through an intact screen. Reconcile all input, output and retained material, and preserve evidence from the failed screen. The worked example deliberately leaves release at zero because capability and missing-fragment evidence remain unresolved. Equipment repair and rescreening throughput are not disposition decisions.
Must the PCQI personally release every affected lot?
The cited provisions assign PCQI performance or oversight to applicable validation and records review; they do not name the PCQI as the required signatory for every lot release. The site should assign a qualified, accountable disposition authority in its procedure. That assignment does not replace required PCQI involvement, corrective-action documentation or an adequate safety basis for release.
Sources
Practical orientation, not legal advice. Rules differ by jurisdiction; your quality and compliance team decides what applies.
The Food Processing Operations Guide
Safe changeovers. Right labels. Every lot traceable.
- The rules and the plan
- Supplier to filled tray
- Allergen changeovers and pack checks
We ask for your name and email so we can handle this request. The full guide then opens on this site, ready to translate, print or save. Privacy policy. Practical orientation, not legal advice; your quality unit decides which rules apply.
 Ultimate
Free guide
The Food Processing Operations Guide
Safe changeovers. Right labels. Every lot traceable.